Advanced Manufacturing Infrastructure
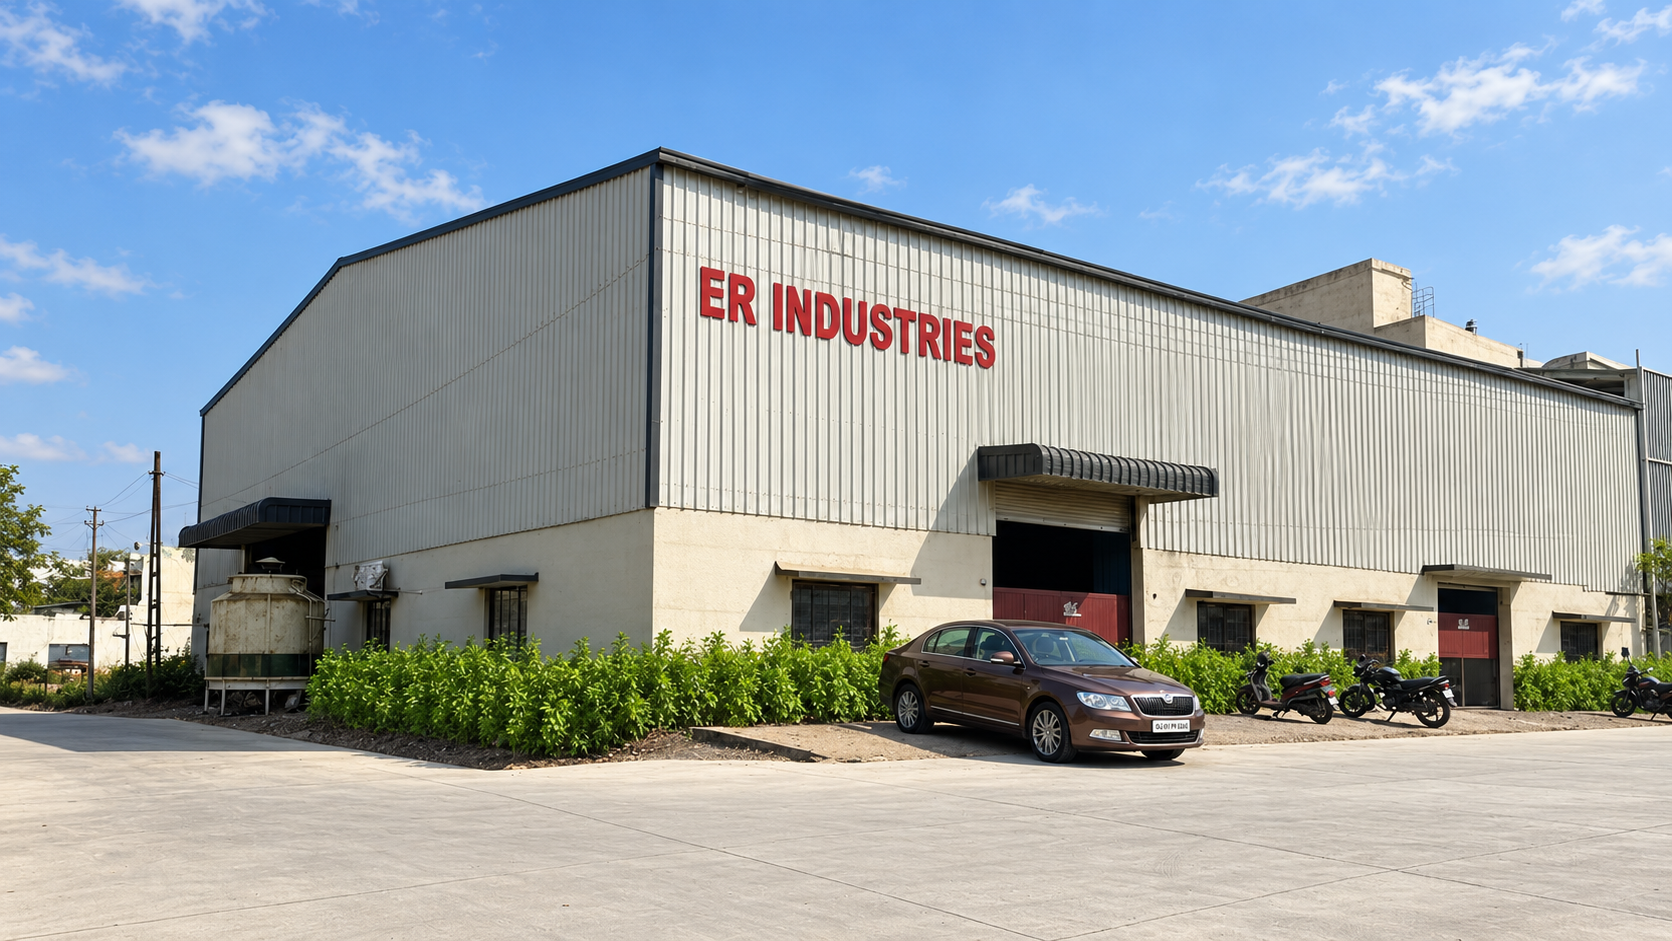
A modernized 18,000 sq. ft. precision facility in Rajkot — engineered for 150 MT/month forging capacity, CNC machining, and zero-defect OEM scale.
FACILITY OVERVIEW
Precision Engineering Built on Solid Foundations
Located at Suvidha Engineering Zone, Rajkot, our facility represents an integrated manufacturing ecosystem designed for high agility, metallurgical precision, and rapid OEM order execution.
Starting with a 1,350 sq. ft. workshop in 2020, ER INDUSTRIES has steadily expanded to a modernized 18,000 sq. ft. plant. In January 2025, we commissioned our state-of-the-art forging line, elevating monthly output to 150 MT per month for both ferrous and non-ferrous components.
150 MT/Month High-Tonnage Forging Lines
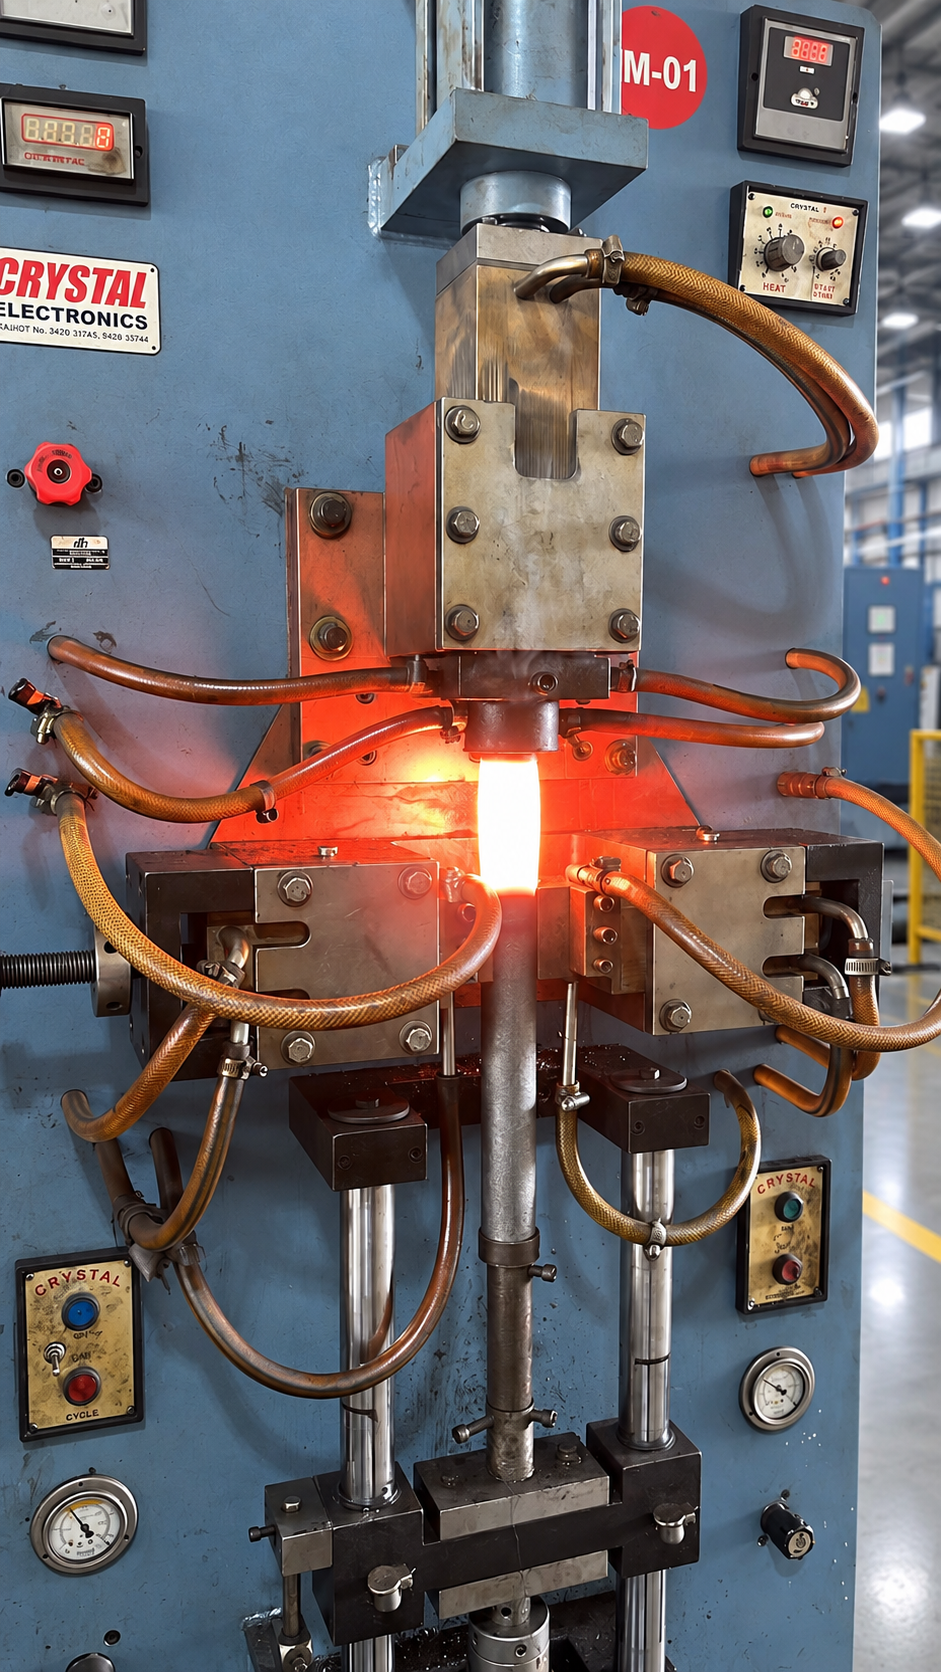
Equipped with high-precision friction screw presses and 50-ton power press lines supported by automated induction billet heating.
In-House CAD/CAM Tooling & CNC Center
Complete closed-die tooling designed in-house with rapid changeovers and high-precision CNC turning/milling cells.
Strategic Global Logistics Connectivity
Direct transport artery to major highways and rapid port dispatch routes (Mundra & Kandla) for worldwide exports.
EXCLUSIVE FACTORY TOUR
Witness Our Active Shop Floor in Motion
Captured live directly inside our 18,000+ sq. ft. facility at Suvidha Engineering Zone, Rajkot — this continuous vertical walkthrough reveals the synchronized operations of induction billet heating, heavy friction screw press strokes, and high-precision component workflow.
Induction Billet Heating
Automated coils delivering 1150°C–1250°C uniform billet heating with zero scaling.
Friction & Power Presses
High-energy mechanical forging strokes forming complex close-die profiles.
Continuous Material Flow
Smooth transfer from heating to press stroke to automated bin collection.
Operator Safety & QA
Pneumatic arm handling, optical temperature audits, and zero-defect tracking.
PRODUCTION WORKFLOW
Vertical Integrated Manufacturing Departments
From raw billet preparation to precision forging, controlled heat treatment, and micron-accurate CNC finishing — executed with rigorous process controls.
 Stage 01
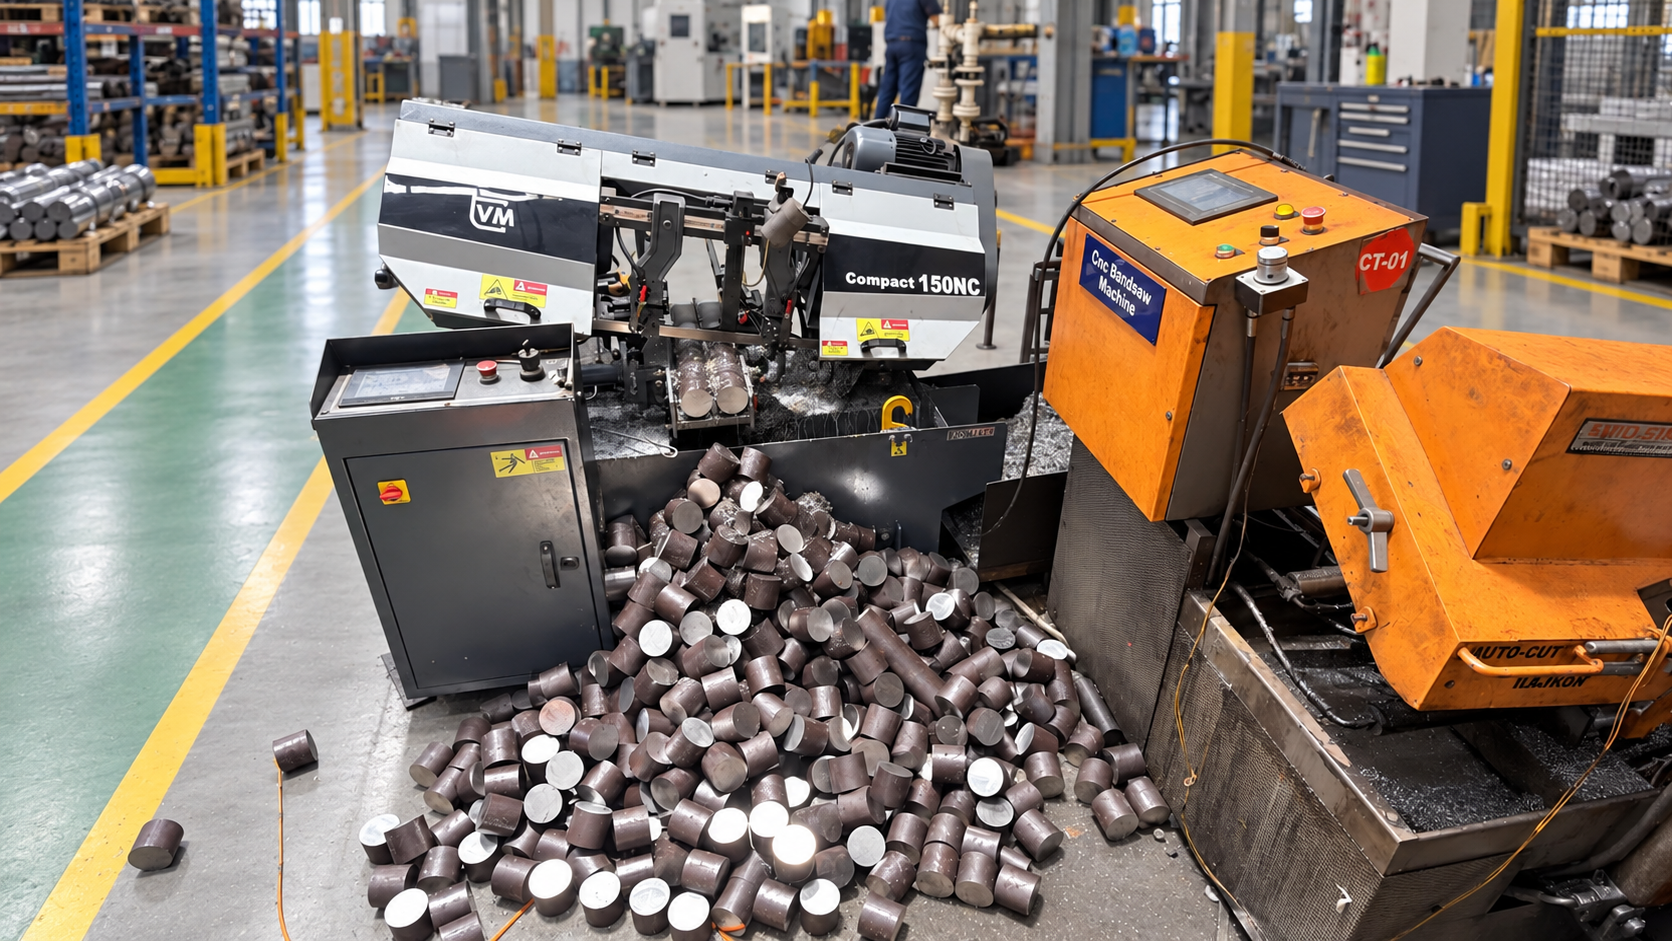
Cutting Shop
Billet Cutting & Preparation
High-speed Compact 150NC band saws and hydraulic shearing units precision-cut round bars into exact billet sizes, minimizing kerf waste and preserving clean square ends.
 Stage 02
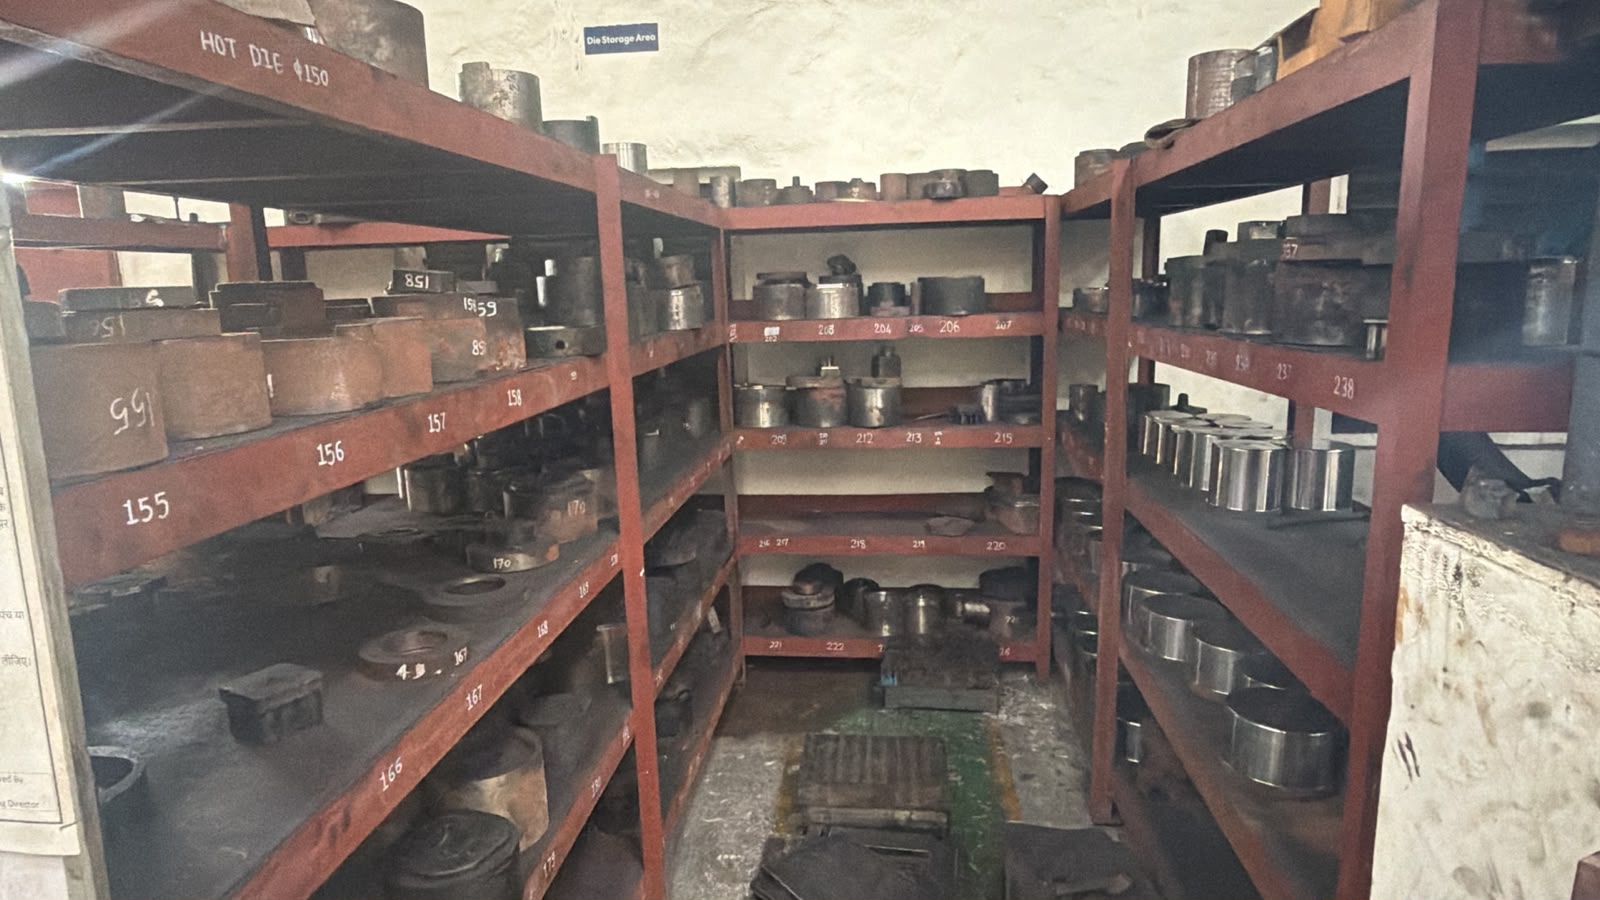
Die Shop
In-House Tooling & Die Design
CAD/CAM engineered closed-die tooling designed and manufactured on-site. Numbered inventory racks allow rapid retrieval, reduced turnaround, and zero tooling mix-ups.
 Stage 03
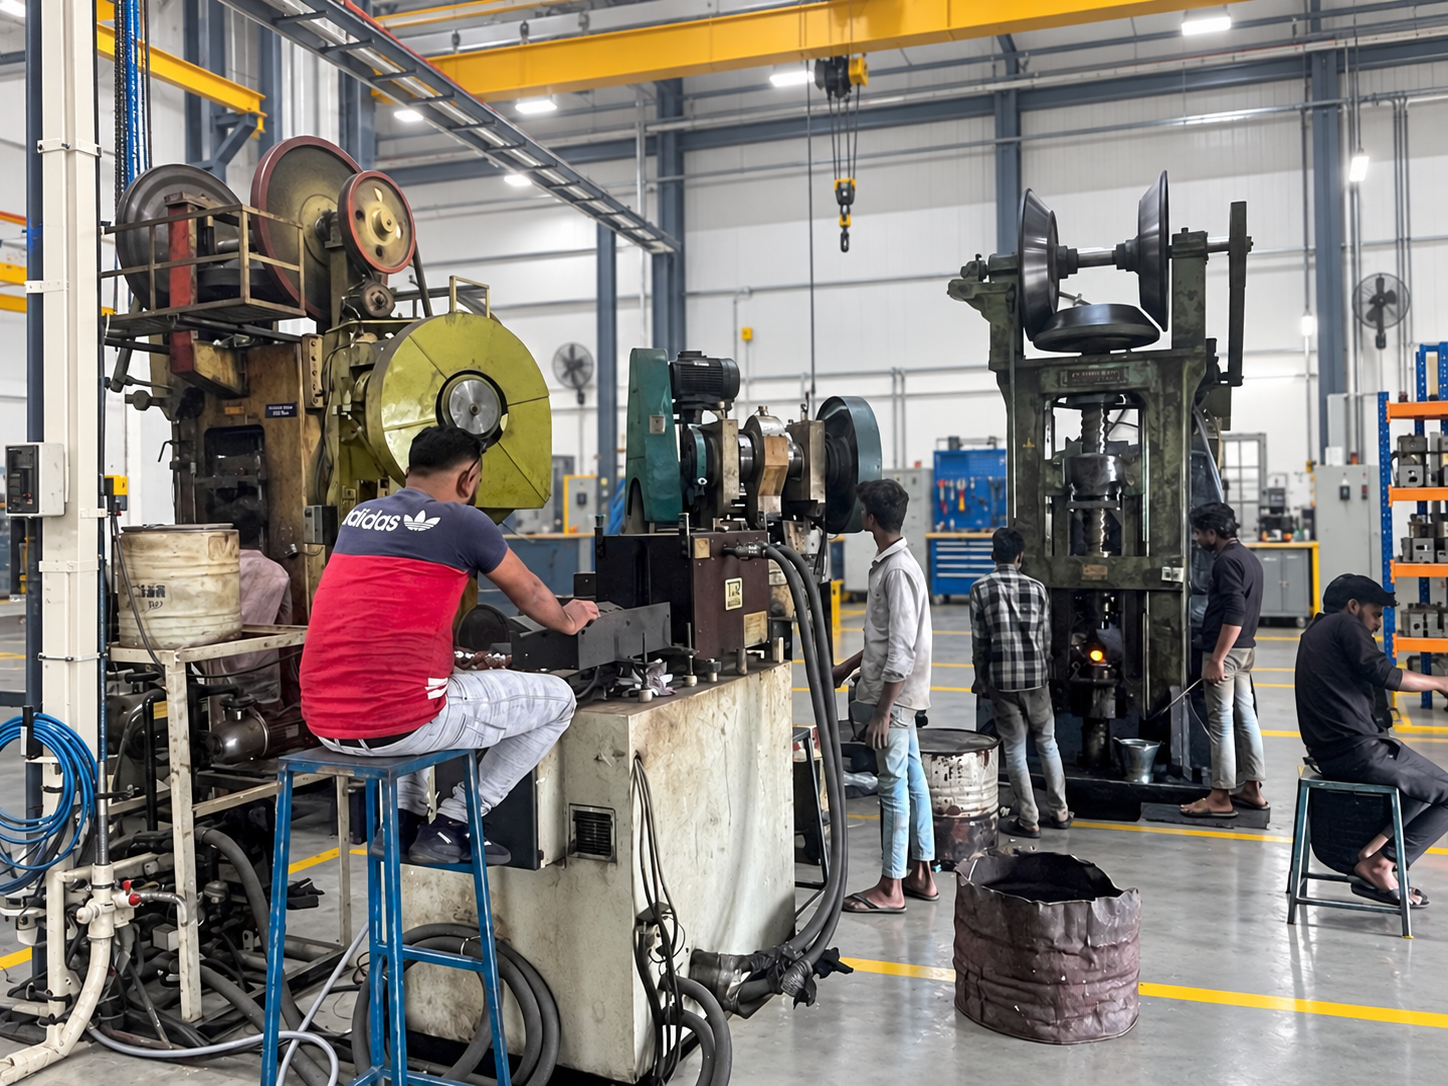
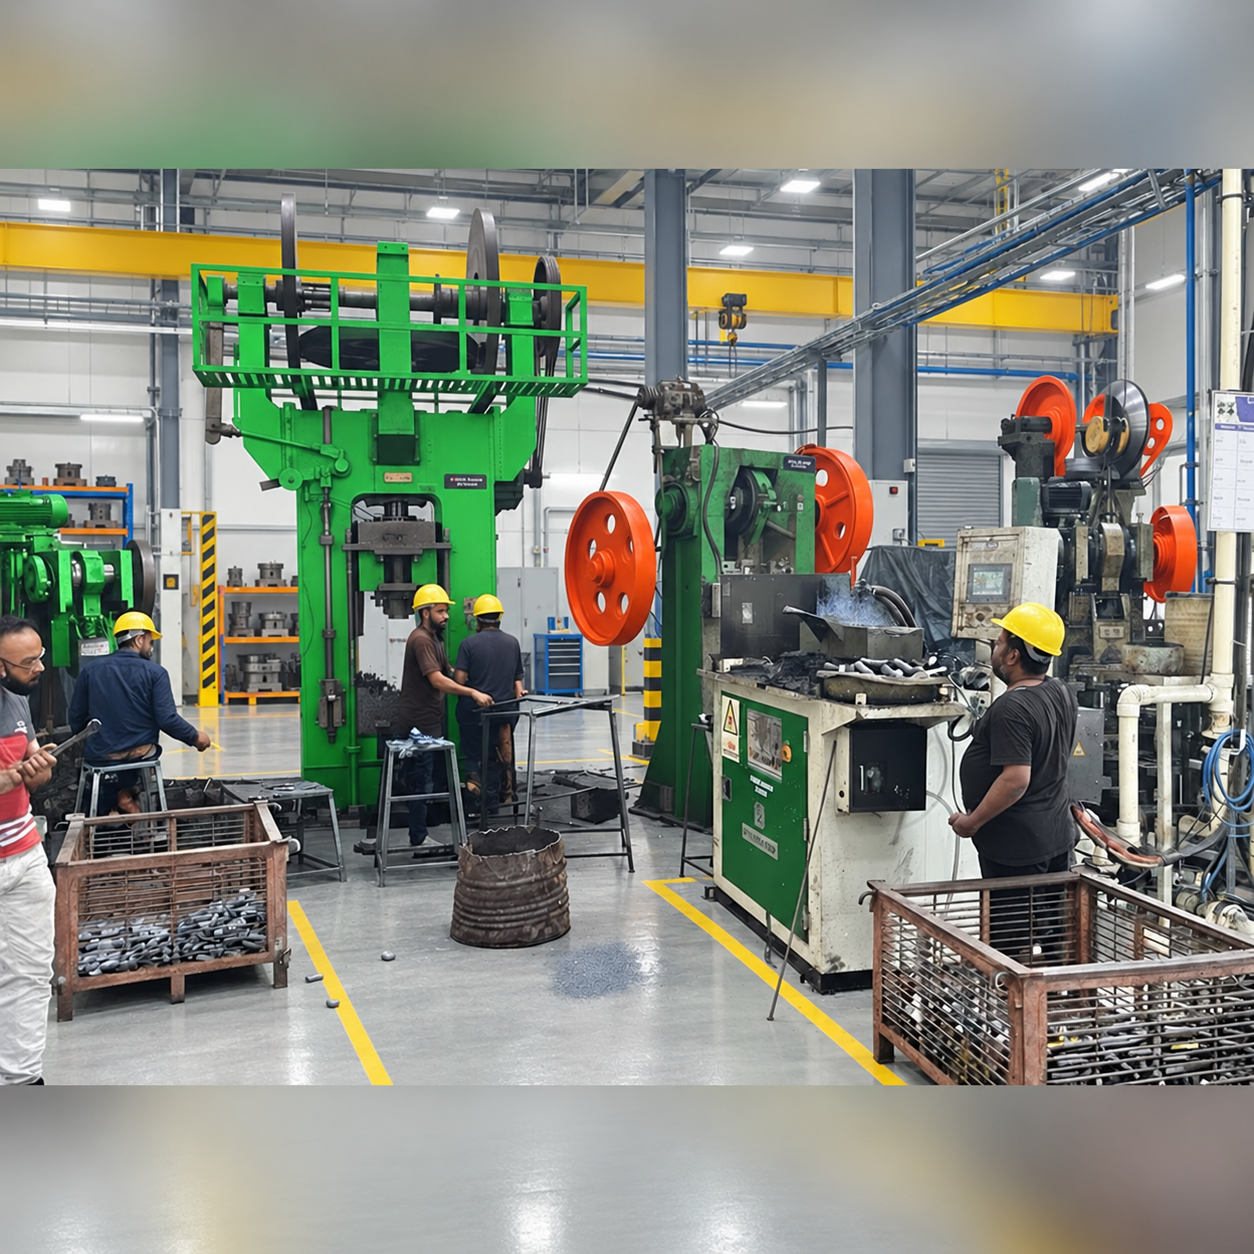
Forging Shop
High-Tonnage Forging Press Lines
Heavy friction screw presses and 50-Ton power press lines with continuous induction billet heating, delivering superior metallurgical grain flow and high mechanical toughness.
 Stage 04
Thermal Lab
Heat Treatment & Metallurgy
Standardized Annealing, Normalizing, Hardening, and Tempering cycles supported by calibrated quenching systems, ensuring target tensile strength, elongation, and microstructures.
 Stage 05
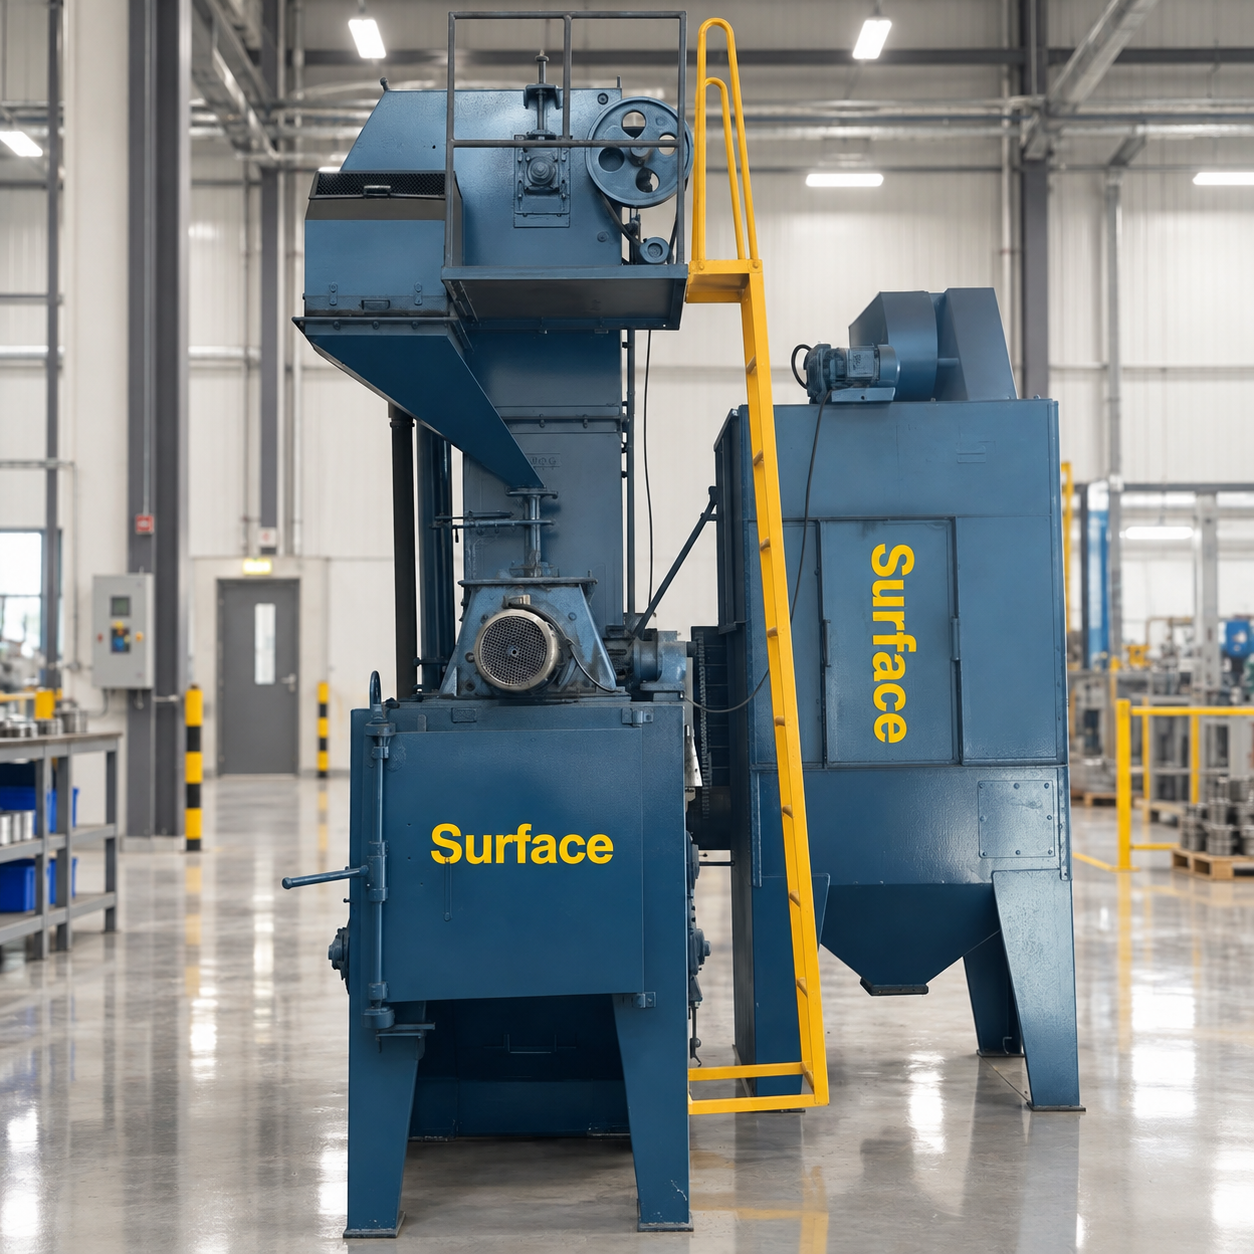
Machining Shop
Precision CNC Machining
Multi-axis CNC turning and milling centers perform secondary operations with micron-level tolerances (IT 4–6), delivering finished, ready-to-assemble OEM components.
 Stage 06
Metrology & QC
Metrology & Zero-Defect NDT Lab
100% optical emission spectrometer chemical validation, Ultrasonic Flaw Detection (UT), Magnetic Particle Inspection (MPI), and CMM dimensional verification before dispatch.
TECHNICAL SPECIFICATIONS
Key Manufacturing Machinery & Equipment
Verified technical specifications across our cutting, forging, tooling, CNC machining, and inspection equipment.
| Department / Process | Key Equipment / Make | Working Capacity | Tolerance / Standard | Quality Verification |
|---|---|---|---|---|
| Raw Billet Preparation | Compact 150NC CNC Band Saws & Shears | Bars up to Ø150 mm | ±0.5 mm Length | 100% Heat-Number Mark Transfer |
| Die & Tooling Hub | CAD/CAM Engraving & Sinking Lines | Dies up to 500 mm | ±0.02 mm Die cavity | Coordinate Optical Inspection |
| Forging Press Lines | Friction Screw & 50-Ton Power Presses | 0.020 to 4.0 kg piece weight | IS:3469 Closed Die Std. | 100% Visual & Weight Audit |
| Billet Heating | Continuous Induction Heating Furnaces | 150 MT / Month throughput | 1150°C – 1250°C | Optical Infrared Pyrometer |
| Precision CNC Machining | Multi-Axis CNC Turning & Milling Cells | Components up to Ø350 mm | Up to ±0.005 mm | CMM & Air Gauging Inspection |
| Metallurgical & NDT Lab | Optical Spectrometer, UT, MPI, Hardness | Complete Ferrous & Non-Ferrous | ASTM, DIN, JIS, BS, IS | 3.1 Mill Test Certificates (MTR) |
Schedule a Physical Factory Audit
We welcome global Tier-1 OEMs, EPC contractors, and procurement heads for technical plant tours, QA audits, and prototype development in Rajkot.